Product
Customizable Steam Condensate Drainage Tank Recycling And Reuse Equipment
In the realm of industrial thermal management, the optimization of energy resources is not merely an operational goal-it is a strategic imperative. The Customizable Steam Condensate Drainage Tank Recycling and Reuse Equipment represents a pinnacle of engineering designed to address one of the most significant yet often overlooked areas of energy loss: the disposal of high-temperature steam condensate. Engineered for heavy-duty industrial applications, this system transcends the functionality of standard condensate collection vessels. It serves as a comprehensive, closed-loop recovery solution that captures, treats, and reintegrates valuable condensate-along with its inherent sensible heat-back into the boiler feedwater system or other process applications. By doing so, it effectively transforms what is typically treated as waste into a high-value operational asset. Uncompromising Customization for Complex Systems Recognizing that no two industrial facilities operate identically, our equipment is built upon a philosophy of total adaptability. Unlike off-the-shelf tanks that often require costly ancillary modifications, our units are fully customizable from the ground up to meet the specific thermodynamic, spatial, and regulatory demands of your facility.
Keywords:
Customizable Steam Condensate Drainage Tank Recycling And Reuse Equipment
Category:
Product Details
Product Attributes
In the realm of industrial thermal management, the optimization of energy resources is not merely an operational goal-it is a strategic imperative. The Customizable Steam Condensate Drainage Tank Recycling and Reuse Equipment represents a pinnacle of engineering designed to address one of the most significant yet often overlooked areas of energy loss: the disposal of high-temperature steam condensate.
Engineered for heavy-duty industrial applications, this system transcends the functionality of standard condensate collection vessels. It serves as a comprehensive, closed-loop recovery solution that captures, treats, and reintegrates valuable condensate-along with its inherent sensible heat-back into the boiler feedwater system or other process applications. By doing so, it effectively transforms what is typically treated as waste into a high-value operational asset.
Uncompromising Customization for Complex Systems
Recognizing that no two industrial facilities operate identically, our equipment is built upon a philosophy of total adaptability. Unlike off-the-shelf tanks that often require costly ancillary modifications, our units are fully customizable from the ground up to meet the specific thermodynamic, spatial, and regulatory demands of your facility.
Key customization parameters
- Material of Construction: Options range from carbon steel for standard applications to high-grade stainless steel (304, 316L) for environments requiring superior corrosion resistance, purity standards (such as food, beverage, or pharmaceutical industries), or handling of aggressive condensate with low pH levels.
- Capacity and Dimensions: Tanks are engineered to match your peak condensate return load, with capacities ranging from small-scale collection units to massive surge tanks capable of handling hundreds of tons per hour. The physical footprint, orientation (vertical or horizontal), and nozzle orientation are designed to integrate seamlessly into existing piping infrastructure.
- Pressure and Temperature Ratings: Whether you are dealing with low-pressure gravity returns or high-pressure, high-temperature flash steam, the tank is designed with appropriate ASME or PED code-stamped pressure vessel construction to ensure safe and reliable operation under specified conditions.
- Integrated Internals: To optimize thermal efficiency, we offer internal engineering features such as flash steam separation chambers to prevent steam hammer, vortex breakers for stable pump suction, submerged inlet pipes to eliminate condensate impingement noise, and internal baffles to maximize thermal stratification.
Advanced Recycling and Reuse Mechanism
The primary function of this equipment is to maximize the Return on Investment (ROI) of your steam system. The process is engineered for efficiency:
1. Capture and Flash Separation: High-temperature condensate enters the tank through a controlled depressurization zone where flash steam is separated. This flash steam can either be vented (if minimal), re-routed to low-pressure heating applications, or captured within the tank to pre-heat incoming makeup water.
2. Thermal Energy Retention: By maintaining condensate at optimal temperatures (typically between 180°F and 212°F), the system drastically reduces the fuel required in the deaerator and boiler. Every 10°F increase in feedwater temperature can result in a 1% fuel savings-a metric that our tanks are designed to maximize.
3. Water Conservation: Condensate is naturally distilled water, free of the total dissolved solids (TDS) found in raw makeup water. By recycling this high-purity water back into the boiler loop, facilities significantly reduce water consumption, chemical treatment costs (for oxygen scavengers and alkalinity builders), and the frequency of blowdown requirements.
Intelligent Controls and System Integration
To ensure reliability and operational transparency, our condensate drainage tanks are equipped with advanced control integration capabilities. The system can be configured with:
- High-Performance Pump Skids: Integrated with ANSI or vertical turbine pumps specifically sized for Net Positive Suction Head (NPSH) requirements, ensuring cavitation-free operation even at near-boiling temperatures.
- Level Control Systems: Utilizing non-contact radar, guided wave radar, or conductive probes, the system automates pump sequencing to maintain consistent tank levels, preventing overflow or dry-run conditions.
- Remote Monitoring: Optional IoT-enabled sensors allow for real-time monitoring of temperature, conductivity, pH, and flow rates, providing facility managers with actionable data to optimize system performance and predict maintenance needs.
Key Benefits
- Enhanced Energy Efficiency: Recovers up to 30% of the energy contained in steam that would otherwise be lost via blowdown or flash steam venting.
- Reduced Operational Expenditure (OPEX): Drastically lowers water bills, sewer discharge fees, and boiler chemical treatment costs by maximizing the return of high-purity, pre-heated condensate.
- Extended Equipment Lifespan: By returning deoxygenated, thermally stable water to the boiler, the system minimizes thermal shock and corrosion, significantly extending the lifespan of boilers, valves, and piping.
- Environmental Compliance: Helps facilities meet sustainability goals by reducing water intake, lowering carbon emissions associated with fuel combustion, and minimizing thermal pollution from wastewater discharge.
- Robust Reliability:Built with heavy-gauge materials, redundant pump options, and failsafe control logic, the system ensures continuous operation even under fluctuating process loads.
Applications
This versatile equipment is ideally suited for industries with high steam consumption, including:
- Food and Beverage Processing: Ensures sanitary conditions while maximizing energy recovery from cooking, sterilization, and drying processes.
- Chemical and Petrochemical:Handles high-pressure condensate with corrosion-resistant materials and robust safety features.
- Pharmaceutical Manufacturing:Provides high-purity condensate recovery essential for clean-in-place (CIP) systems and sterilization.
- Pulp and Paper:Manages large volumes of flash steam and condensate with high-capacity, heavy-duty configurations.
- Textile and Automotive:Supports consistent process heating with reliable condensate management under varying load conditions.
Main Material
Stainless Steel、carbon steel、Nickel and nickel-based alloys、Titanium & titanium alloys、Copper&copper alloys、Zirconium&zirconium alloys, etc...
Production Capacity
| ANNUAL OUTPUT (If device dia is more than 1000 mm, max lifting weight is 100 ton) | |||||||
| YEAR | 2017 | 2018 | 2019 | 2020 | 2021 | 2022 | 2023 |
| REACTOR | 129 | 133 | 177 | 180 | 220 | 303 | 339 |
| HEAT EXCHANGER | 119 | 132 | 153 | 210 | 260 | 375 | 452 |
| COLUMN | 112 | 128 | 177 | 147 | 180 | 285 | 317 |
| STORAGE TANK | 95 | 150 | 162 | 142 | 203 | 300 | 556 |
| SPECIAL EQUIPMENT | 190 | 106 | 98 | 119 | 138 | 350 | 378 |
| TOTAL | 645 | 647 | 707 | 798 | 1001 | 1613 | 2042 |
Features
High-Quality Construction: Fabricated from the finest premium-grade materials, this vessel is engineered to endure extreme operational conditions while preserving its structural integrity, offering reliability and longevity in even the toughest environments.
Precision Engineering: Expertly designed to manage both positive and negative pressure scenarios, making it the perfect choice for a diverse array of industrial applications, ensuring versatile and adaptable usage.
Rigorous Testing: 100% X-ray testing to ensure our products meet international standards, delivering leak-free performance and offering quality assurance.
Strong adaptability: Engineered to be applicable to a diverse range of materials and working conditions, showcasing versatility and efficiency across various operational environments.
Supply Ability & Additional Information
Supply Ability: 15-90 days
Certificate: ISO, ASME, GOST, others
Production Capacity:500 Pieces/Year
Transportation: Ocean,Rail transport,Land,Others
Payment Type: T/T, L/C, D/P,Bank Guarantee,Others
Incoterm: FOB, FCA, CFR, CIF, FAS, DDP, DAP, Others
Specification:Customized on Request
We'll help you configure a system that meets all of your research needs.
Packaging & Delivery
Selling Units: Set/Sets
Package Type: asked by buyer
Shipping Preparation: Pickling and passivation for stainless steel parts
Departure: No.9 Yangtes south Road ( No.1 Bonded Zone ), Yangzhou City, Jiangsu Province, China.
Company Overview
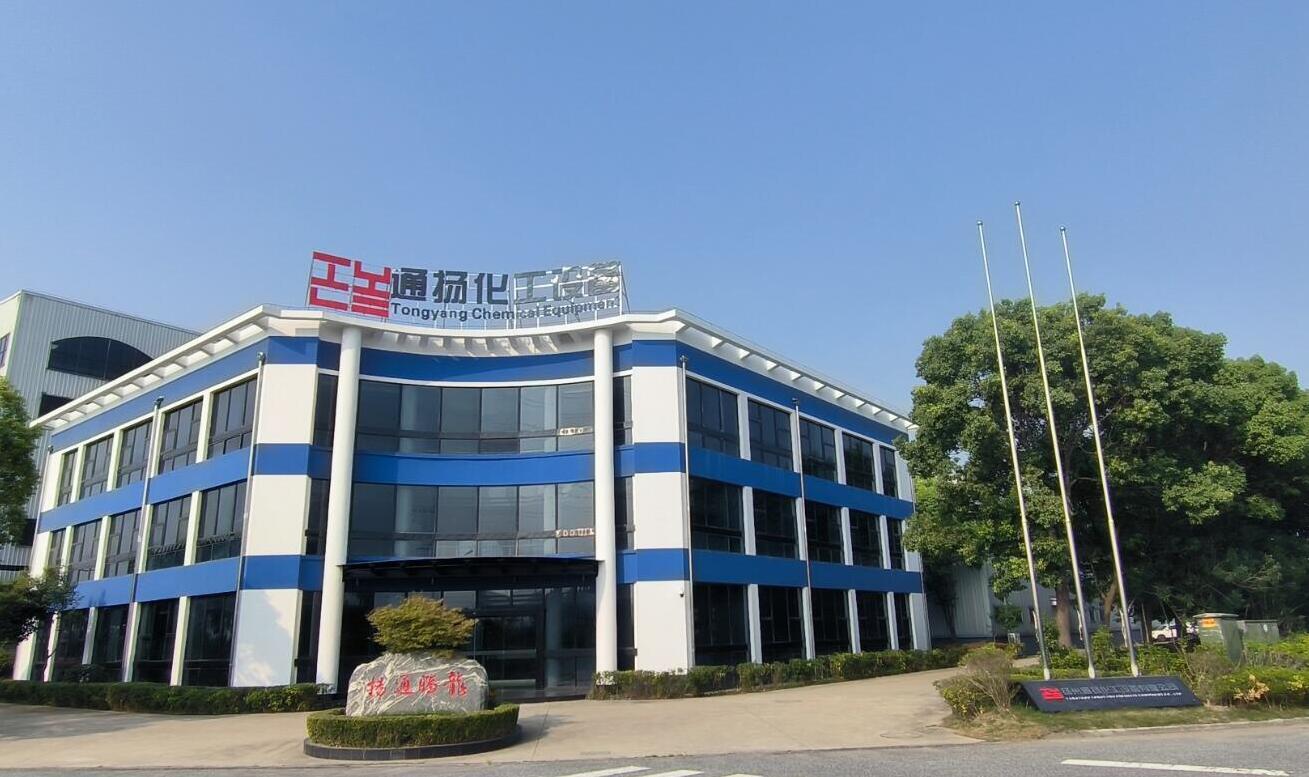
Founded in 1990, TongYang is a professional company specializing in developing and manufacturing chemical machinery and equipment for customers ,It has manufacturing license of grade A2 (the third type of pressure vessel) issued by state general administration of market supervision, license Key: :TS2210D94-2023. Tongyang has always been committed to the research and development, production, application of chemical machinery and equipment in fine chemical, petrochemical, food, biological and pharmaceutical industries. Our technology in develop distillation tower and separation equipment attain domestic leading level, Keep pace with international advanced level.
Provide turnkey projects
Our team can provide you with turnkey engineering, you do not have to worry about the installation is not professional, we will complete the installation and debugging according to your specific requirements, at the same time, a professional training, to solve your worries.
Competitive Advantage
Abundant experience: more than 30 years experience in non-ferrous metal cladding and production;
Technical consulting service: technical consulting on material, welding, NDE, Welding, Heat treatment ;
Independent inspection service; in-process inspection, final inspection; Hydrostatic testing etc;
Transportation: have own export license, Yangzhou Port and Shanghai Port , 2.4 kilometers away from Yangzhou Port and 226 kilometers away from Shanghai Port.
Varieties of manufacturing standards to meet the needs of the global market
GB150-2011;
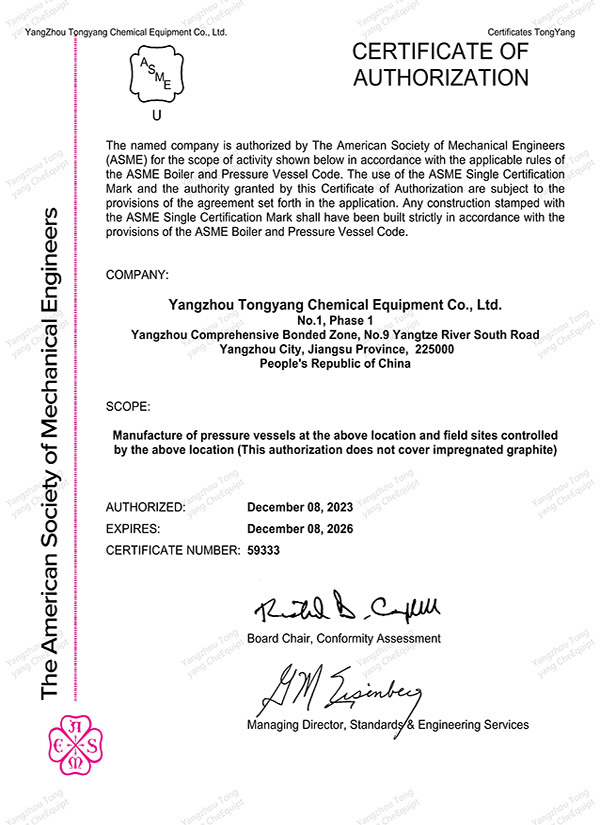
ASME U, U2 Certificate;
GOST 34347;
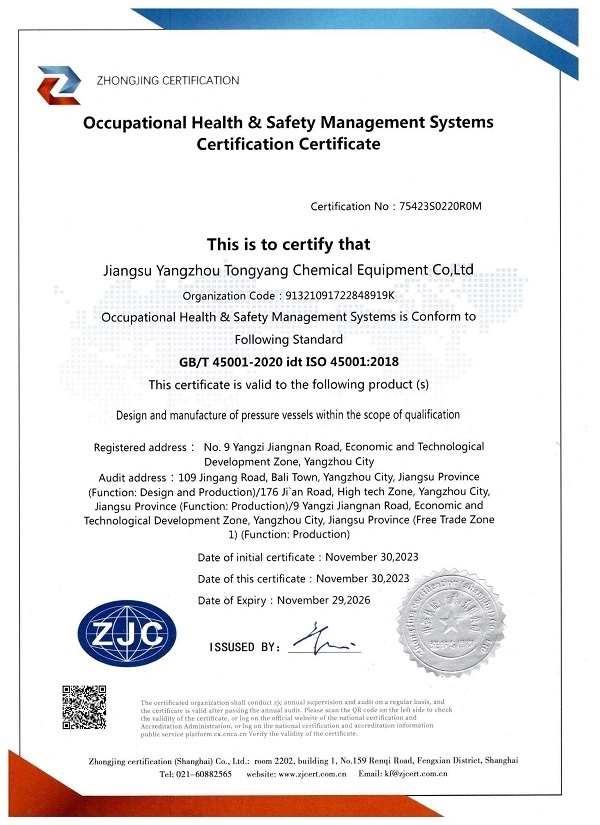
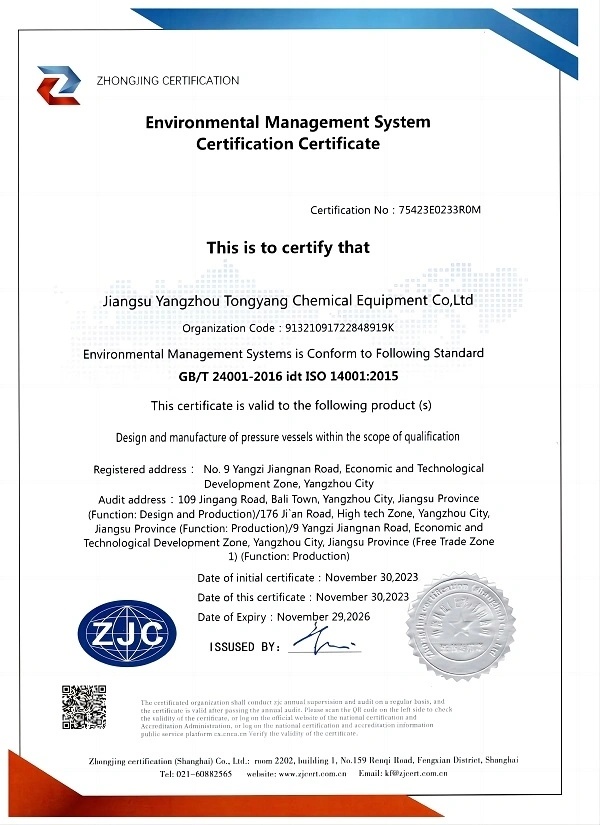
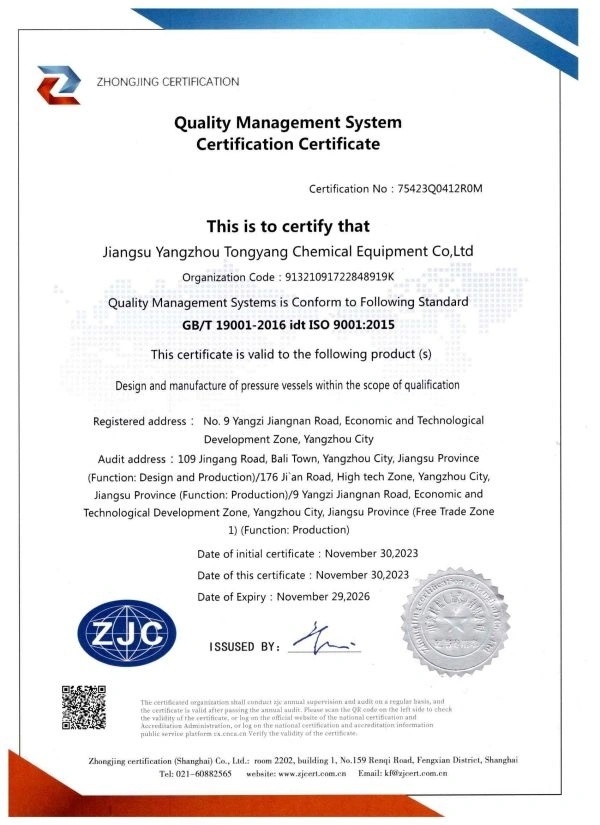
ISO14001 , ISO 45001, ISO 9001;
ASME SEC VIII DIV.1,ASME SEC VIII DIV.2 ; f.PED 97/23/EC with CE certificate;
Workshop Photos

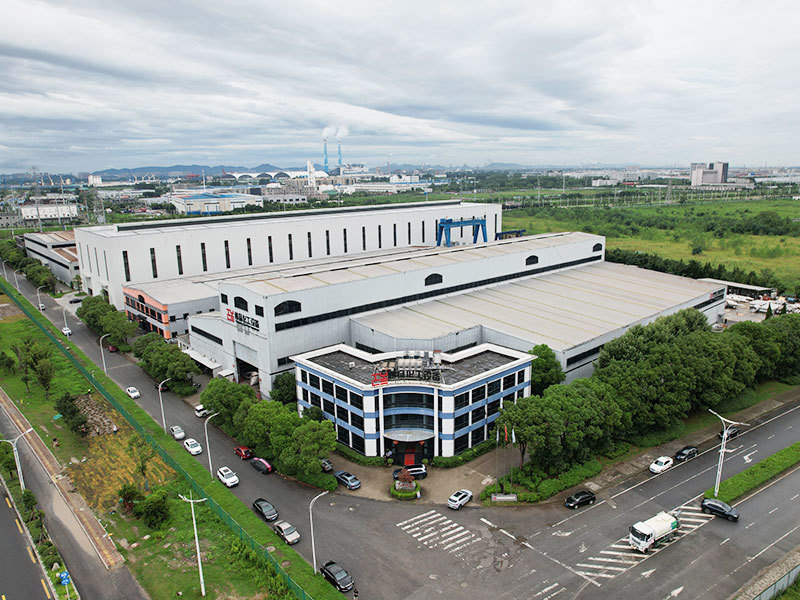
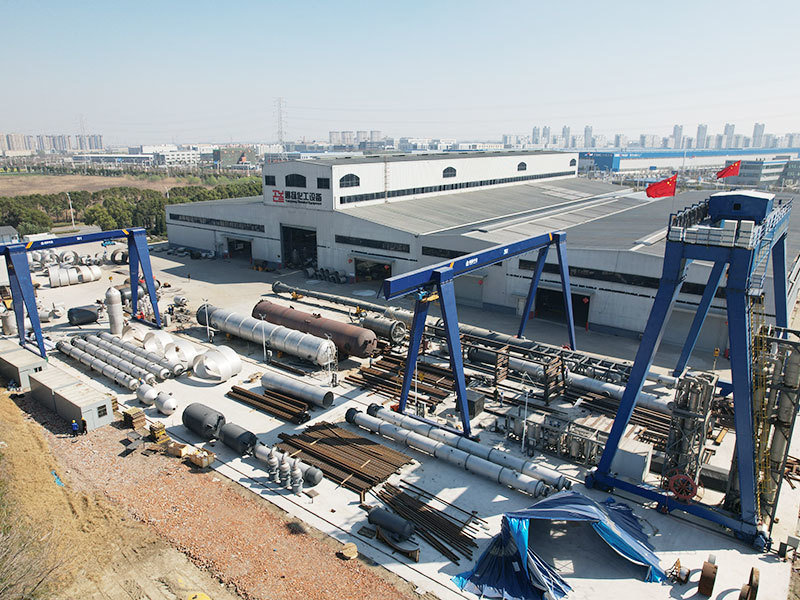
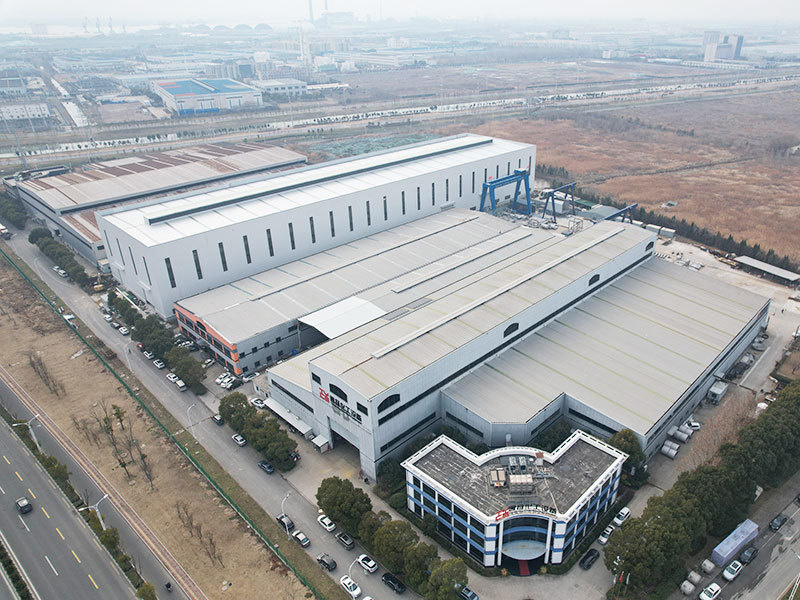
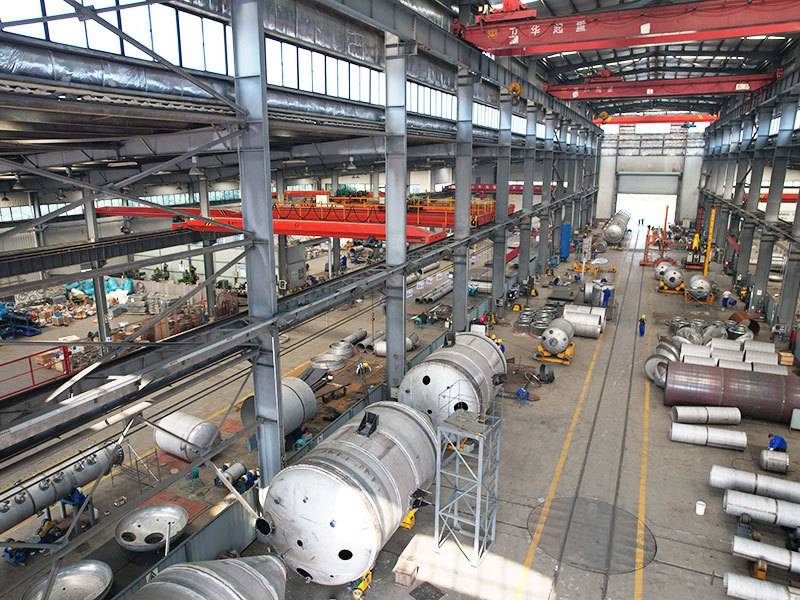
Production workshop
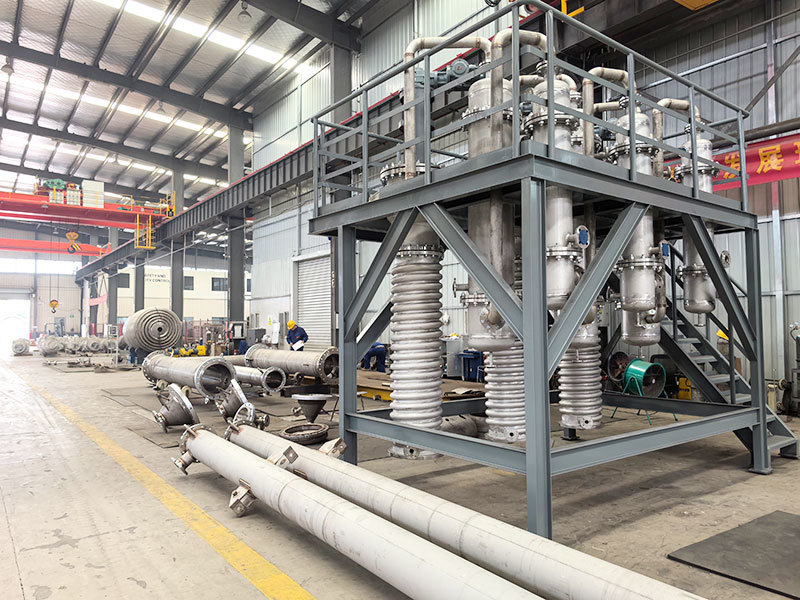
Production workshop
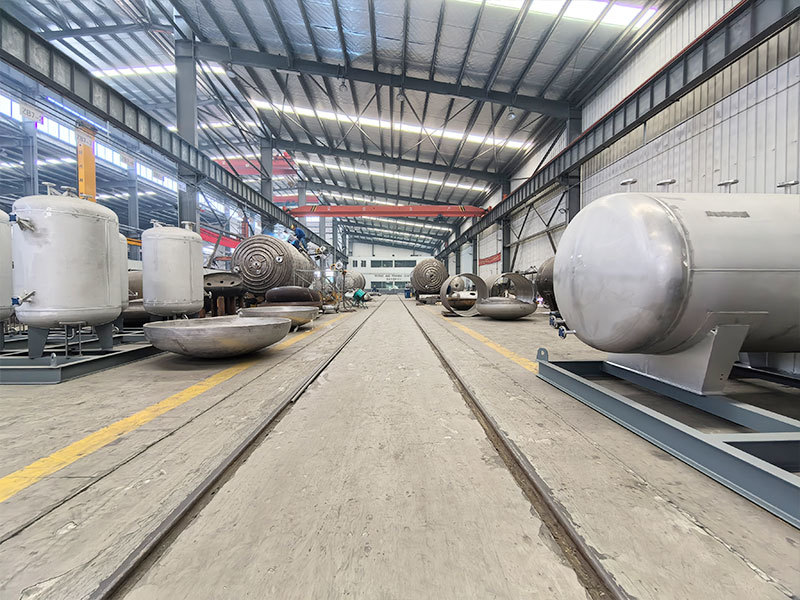
Production workshop
Production Certification


Consultation
Address
No. 9 Yangtes south Road (No. 1 Bonded Zone), Yangzhou, Jiangsu China


Copyright©2023 Yangzhou Tongyang Chemical Equipment Co., Ltd.